Tool Setter Position
The Tool Setter Position section sets where your tool setter is, in MACHINE COORDINATES. At the end of every tool change that loads a tool, the spindle rises to Z Clearance, moves to this X and Y, and calls Tn M6 for the new tool n. The Masso then measures the tool itself, with its own tool setter settings.
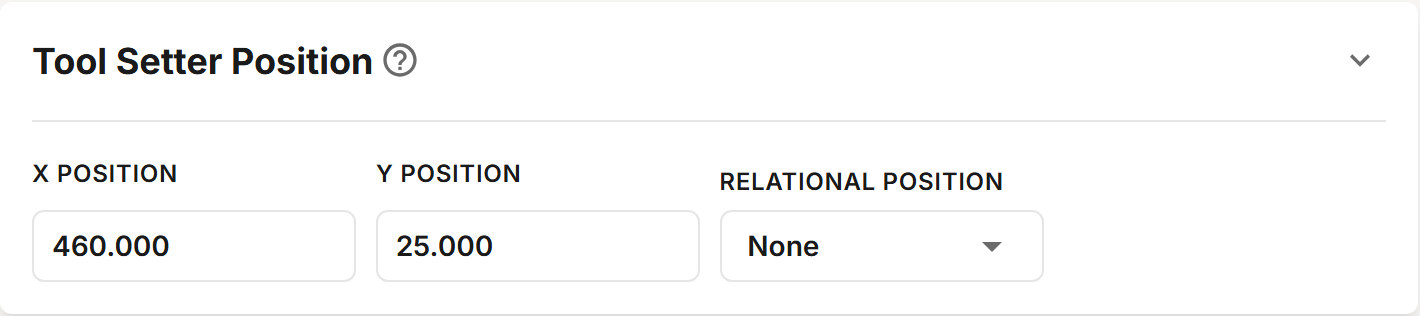
Fields
| Field | Description |
|---|---|
| X Position | MACHINE COORDINATE X of the center of the tool setter. |
| Y Position | MACHINE COORDINATE Y of the center of the tool setter. |
| Relational Position | Where the tool setter sits relative to the magazine. Shown only on a profile with a Linear magazine. |
A Masso G3 profile has no Tool Measurement section: how far the spindle probes, and how fast, are set on the Masso.
Relational Position
| Option | Description |
|---|---|
| None | The tool setter is on the table, outside the magazine. This is the default. |
| Internal | The tool setter is mounted on the magazine. |
| For older magazines with the tool setter in the first or last pocket. X Position and Y Position are greyed out and follow that pocket. |
On a magazine with a dust cover, the placement decides when the cover closes:
- With Internal, the cover stays open while the tool is measured.
- With any other placement, the cover is closed before the spindle moves to the tool setter.
The Masso also moves to its tool setter outside a tool change, for example for Auto Tool Zero after homing, and the subroutines do not open the dust cover then. Most Masso users mount the tool setter outside the magazine.
Setting Up the Masso
The Masso measures each tool when the subroutine calls Tn M6. Set the Masso up so that call measures the tool at this position and goes nowhere else:
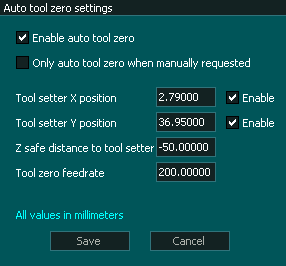
Set the Masso's Auto Tool Zero position, in F1 SETUP, to the same X and Y as this section.
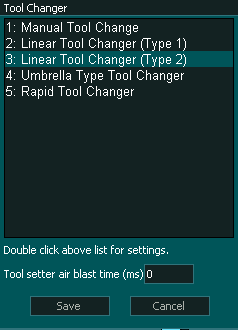
Set the same position in the Masso's Linear Tool Changer (Type 2) settings, in F1 SETUP.
Give every tool its own slot, and set each slot's X and Y to the tool setter position. Every tool needs a slot, manual tools included.
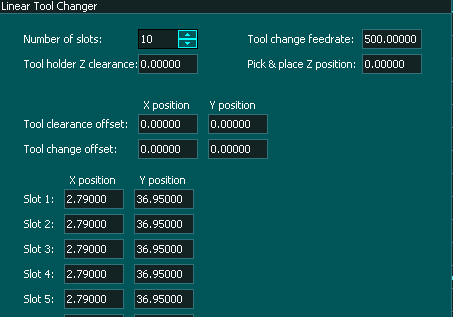
Add each tool in F4 TOOLS & OFFSETS, with its slot. A tool with no slot stops the Masso with "TOOL TO LOAD NOT SET TO ANY SLOT" or "TOOL TO UNLOAD NOT SET TO ANY SLOT".
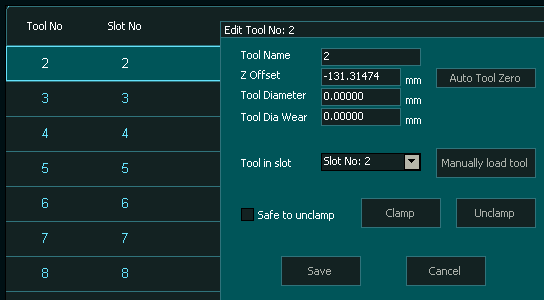
The Masso measures a tool on
Tn M6only when it does not already hold that tool as its current tool. If a tool change ends without the tool touching the tool setter, the Masso already showed that tool as loaded.