Getting Started
Masso G3 runs automatic tool changes from programs and subroutines that your profile generates. You set up the profile in the web app, generate the files, and load them onto your Masso G3. Every tool has its own subroutine: M98 P631 changes to tool 1, M98 P632 to tool 2, and so on. Each one unloads the tool in the spindle, loads the new tool, checks both with the IR beam, and then moves to your tool setter and calls T1 M6 (for tool 1), so that the Masso measures the tool.
The Masso does not tell the subroutines which tool is in the spindle. The profile's Pocket Tracker keeps track of it instead, on pairs of Masso outputs wired back to Masso inputs. See Pocket Tracker.
What You Need
- A RapidChange ATC magazine, Linear or Modular, and the activation code that came with it.
- A Masso G3 controller.
- The magazine's IR sensor wired to a Masso auxiliary input, and, if your magazine has one, the dust cover wired to a Masso auxiliary output. See Tool Detection and Dust Cover.
- Free auxiliary inputs and outputs for the Pocket Tracker: one output wired to one input per pair. A magazine with up to 6 pockets needs 3 pairs, up to 14 pockets 4 pairs, and up to 30 pockets 5 pairs. Ensure Sync, the default, adds one more pair. See Pocket Tracker.
- A tool setter, set up as the Masso's own tool setter for Auto Tool Zero. See Tool Setter Position.
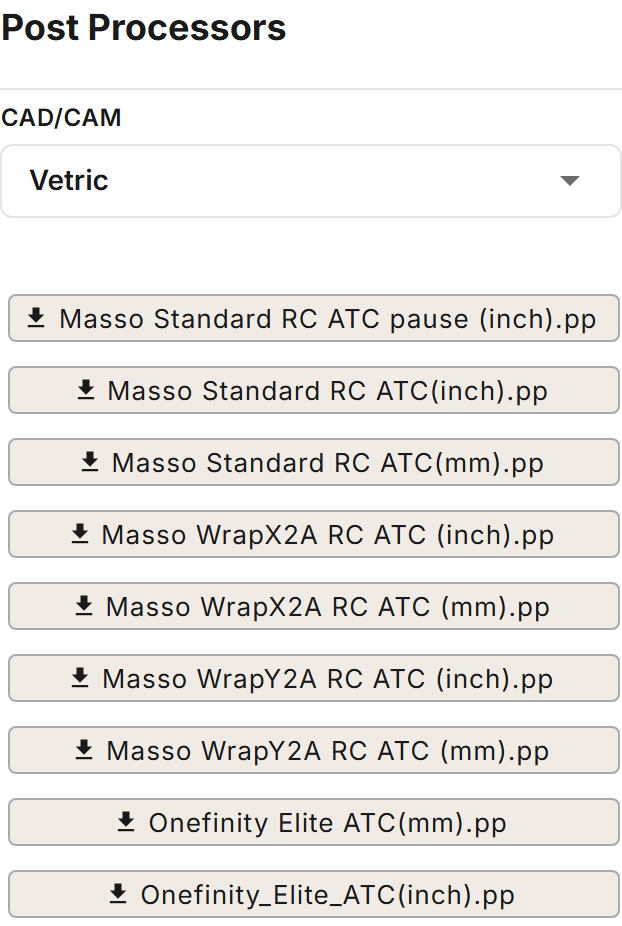
- A Masso post processor for your CAM software, which writes each tool change in your G-code as a call to the tool's subroutine. Download it from the profile's Post Processors card.
Setting Up
1. Activate the magazine and create the profile
In the web app, choose Activate a Magazine. The Activate New Magazine dialog walks you through:
- Enter Activation Code: the code you received with your magazine.
- Select Activation Type, if offered: activate it as a standalone magazine, or extend a magazine you already have.
- Select Motion Control: choose Masso G3.
- Select Initial Data, if offered: Create New Profile, or add the magazine to an existing Masso G3 profile to use more than one magazine.
- Select Setup Units: Imperial (Inches) or Metric (Millimeters).
- Enter Profile Name: up to 30 characters.
When you finish, the new profile opens.
2. Work through the profile's sections
The profile is laid out on tabs: Magazine (Magazines when the profile holds more than one), Tool Setter, Global and Detail. Every position is entered in MACHINE COORDINATES.
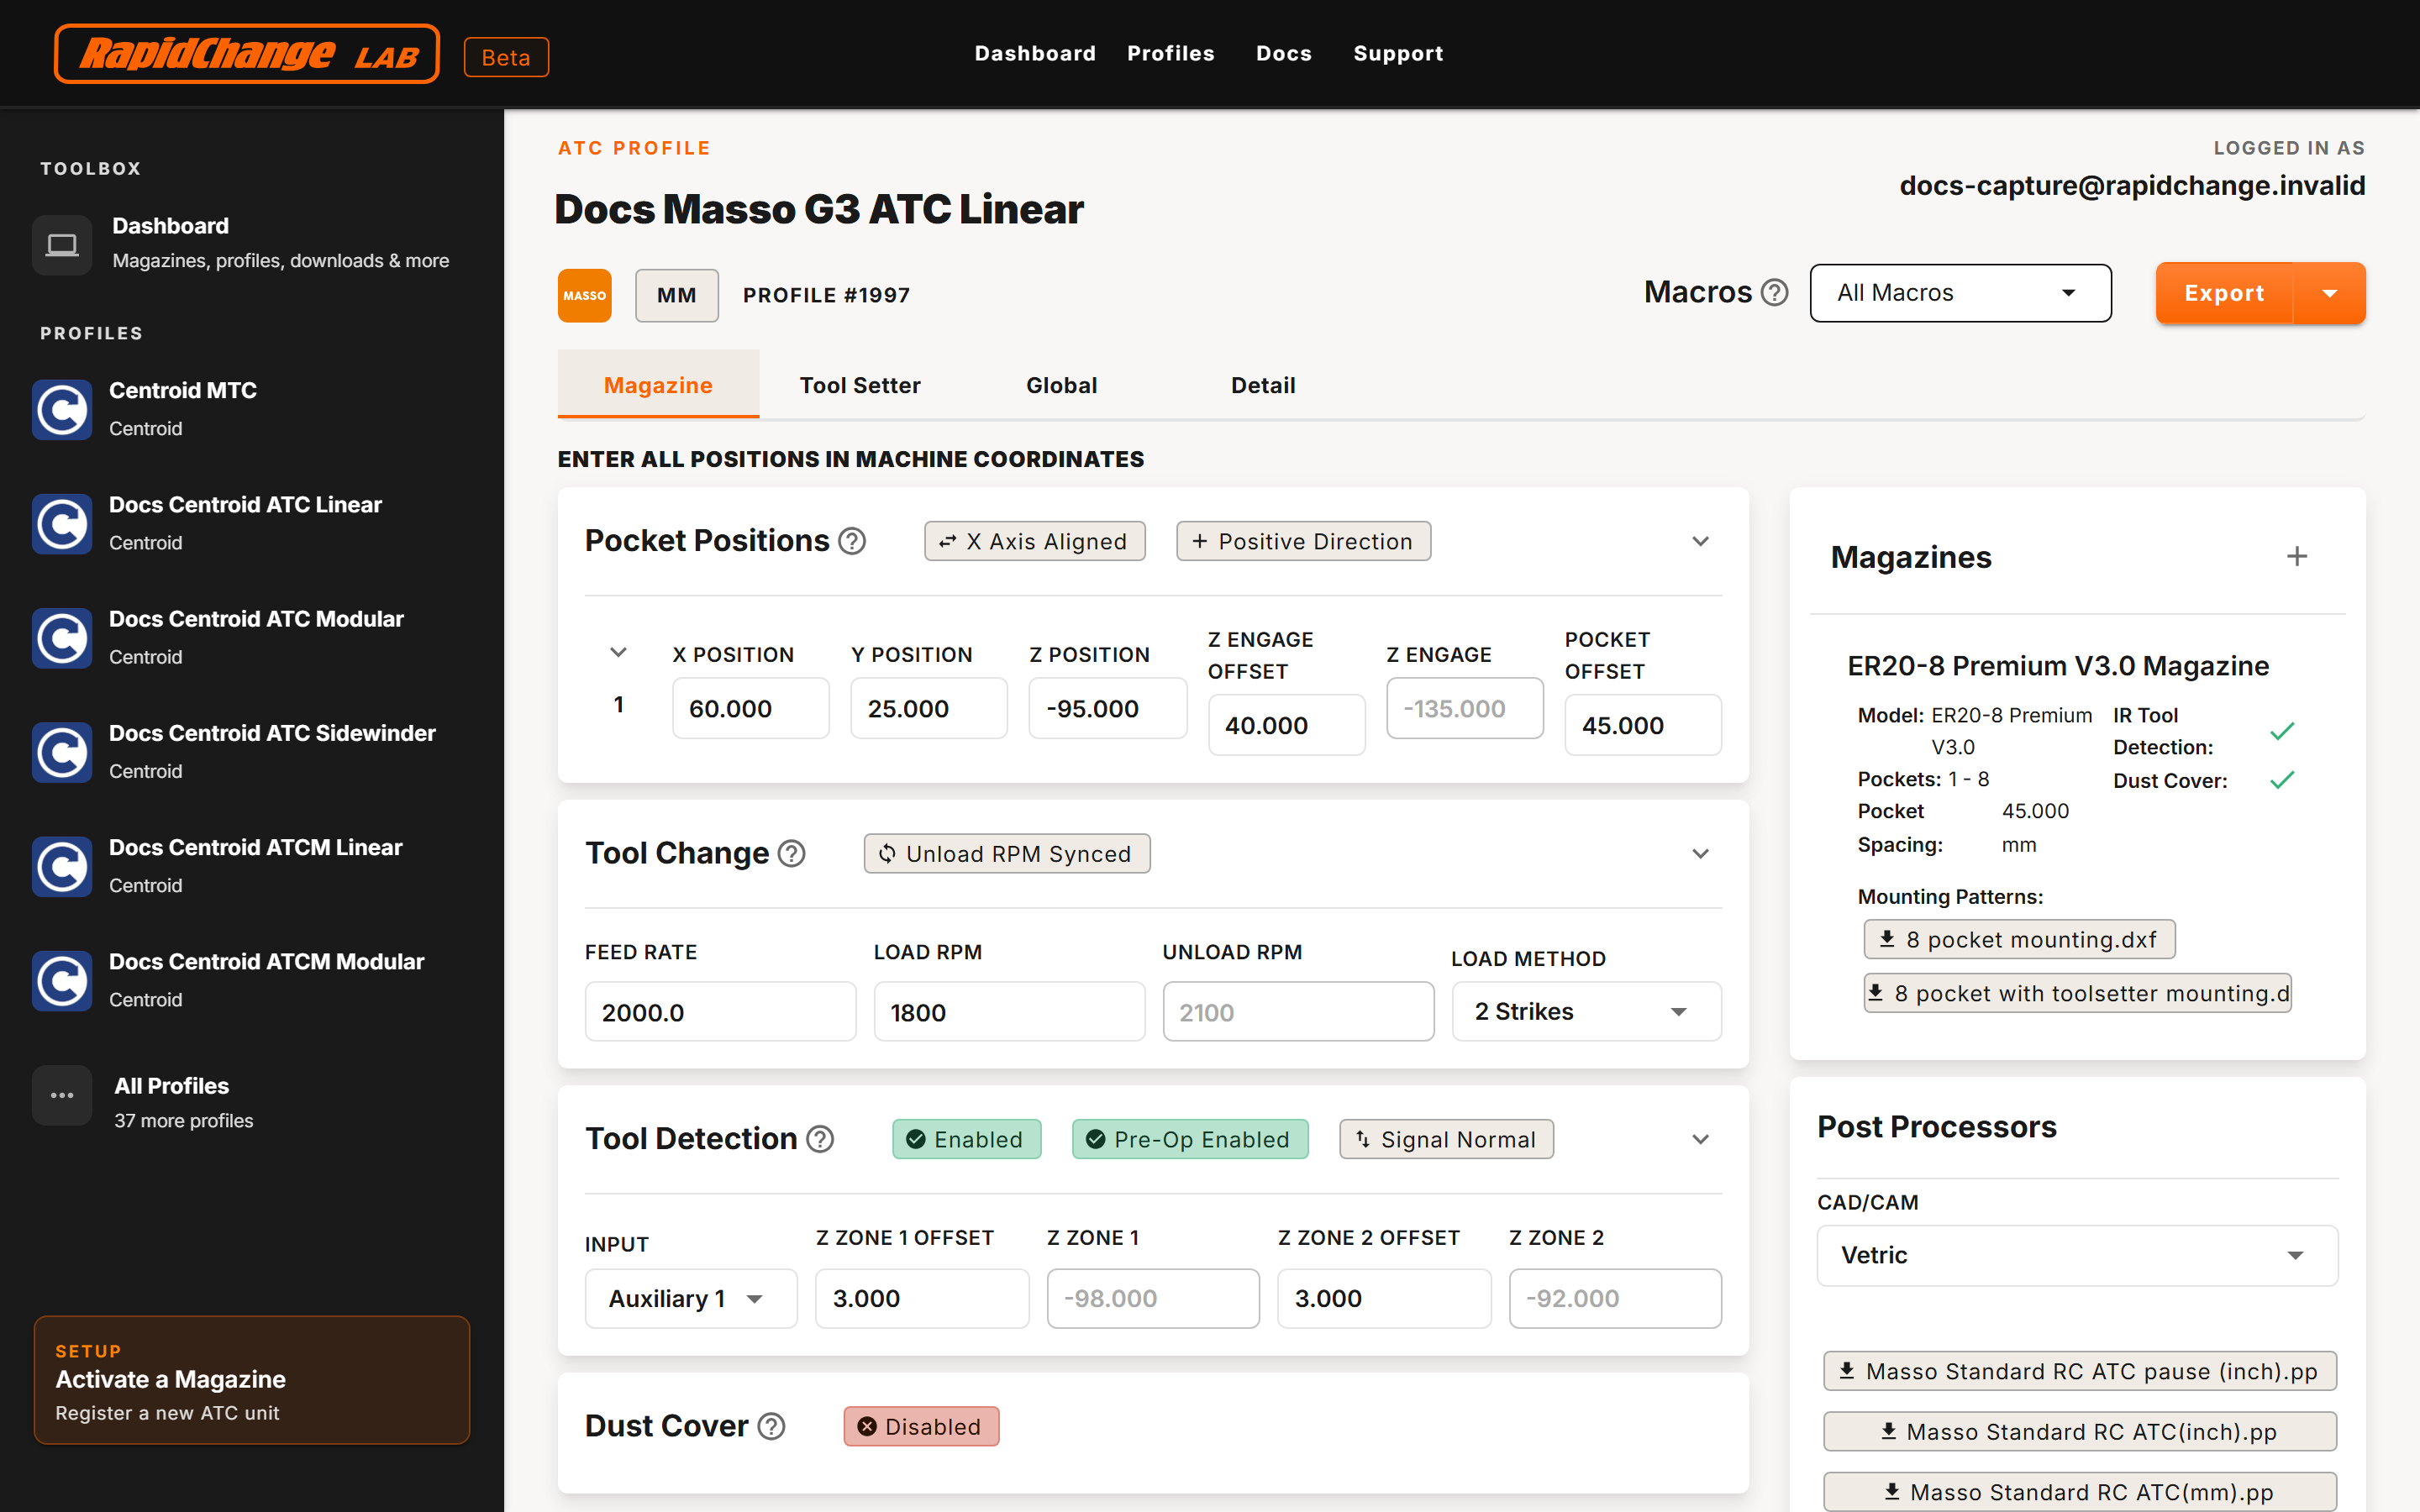
Set up the sections in this order. Each has its own help page.
- Tool Detection (Magazine tab): select the IR sensor's Input. Find Z Position reads the beam through it.
- Move Heights (Global tab): set Z Clearance before anything else moves.
- Pocket Positions (Magazine tab): set X Position and Y Position. Z Position comes from Find Z Position in step 4.
- Find Z Position: see below.
- Tool Change (Magazine tab): spindle speeds, feed and strikes.
- Dust Cover (Magazine tab): enable it if your magazine has one, and choose an output that the Pocket Tracker does not use.
- Tool Setter Position (Tool Setter tab): where tools are measured.
- Manual Position (Global tab): where tools are changed by hand.
- Pocket Tracker (Global tab): match each I/O pair to the auxiliary input and output you wired together.
- Tools (Global tab): the tools you will call, and the pocket each one lives in. A new profile has a tool for each pocket.
On a profile with more than one magazine, select each magazine in the Magazines card and set up its Pocket Positions, Tool Change, Tool Detection and Dust Cover.
3. Generate the files
The Macros control is in the profile's header. Choose All Macros or Find Z Position from its list, then Export or Download:
- Export writes the files, unzipped, into a folder you choose. It is offered only when your browser supports it.
- Download saves them as a zip. Unzip it before you copy the files to the Masso.
All Macros is unavailable while the profile has errors: the box under the control reads "Profile has errors - macros unavailable" and lists them. Find Z Position stays available. A profile needs at least two tools in Tools.
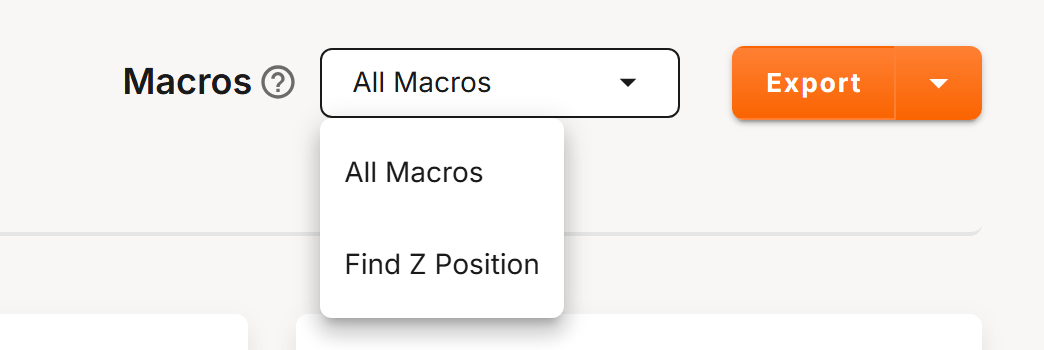
All Macros holds two kinds of file:
- Subroutines, which your G-code and the programs call:
63n.ncfor each tool n, and601.nc, the check that the beam is clear before a tool change. - Programs, which you run from the Masso: Load Tool n, Unload Current Tool, the Sync programs, Show Active Pocket, Pocket Tracker Test, Tool Change Test and Find Z Position.
See Macros for each file.
Copy the subroutines and the programs to the Masso.
Generate the files again, and replace them on the Masso, every time you change the profile. The files hold the profile's values; the Masso does not read the profile.
4. Find Z Position
Find Z Position is available before the profile is complete, because Z Position is one of the values the profile needs.
- Generate Find Z Position, and copy both of its files,
Find Z Position.ncand its subroutine600.nc, to the Masso. - With a tool in the spindle, lower it into the first pocket far enough to break the IR beam.
- Run the Find Z Position program. If the beam is not blocked when it starts, it stops with "IR beam is clear. Adjust and retry".
- The spindle rises in 0.1 mm steps until the beam is clear, then stops with "Record MACHINE Z Position". If the beam is still blocked after 3,000 steps, it stops with "Beam still obstructed. Run again".
- Read the machine-coordinate Z from the Masso, enter it as Z Position in Pocket Positions, and save.
The full procedure, and the method for magazines without an IR sensor, are in Pocket Positions.
5. Your first tool change
- Finish every section until the profile shows no errors, then generate All Macros and copy the files to the Masso.
- Run Pocket Tracker Test. It switches each I/O pair's output on and off and checks that its input follows. It ends with "Success! Pocket Tracker is working", or names the pair that failed, such as "Pair 2 Failure: In 3 Out 3".
- With the spindle empty, run Sync Empty Spindle to record that no tool is in the spindle. Sync again whenever the Masso has been switched off. See Pocket Tracker.
- Put a tool in pocket 1.
- Run Load Tool 1, with your hand near the E-stop. Watch the spindle travel to pocket 1, load the tool, check it with the beam, and move to the tool setter to measure it.
- Run Unload Current Tool to watch an unload. The tool returns to pocket 1 and the spindle is left empty.
Before the first tool change, check Z Clearance, Z Position and the pocket positions. Every move to a pocket is made in machine coordinates from these values.
6. Your CAM software
Download the post processor for your CAM software and units from the Post Processors card on the profile. Choose your software under CAD/CAM to see its files.
Where to Go Next
Each section of your profile has its own page:
- Pocket Positions: where the magazine is, and finding Z Position.
- Move Heights: Z Clearance and the height between pockets.
- Tool Change: spindle speeds, feed and strikes.
- Tool Detection: the beam checks.
- Dust Cover: enable it if your magazine has one.
- Tool Setter Position: where tools are measured.
- Manual Position: where tools are changed by hand.
- Tools: the tool library.
- Pocket Tracker: the I/O pairs and syncing.
- Macro Hooks: your own steps before and after a tool change.
- Macros: every file and what it does.