Tool Detection
The RapidChange ATC uses an infrared beam to check that each unload and load has worked. The IR sensor must be wired to an input on your controller and selected here.
The section is shown only for a magazine with IR tool detection.
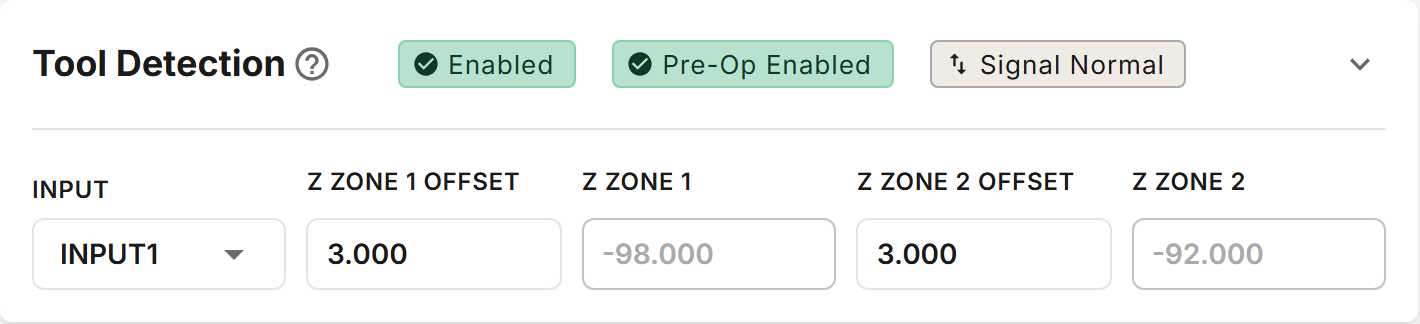
Chips
The chips in the section's header:
| Chip | Description |
|---|---|
| Enabled / Disabled | Turns tool detection on or off. A new profile starts with it Enabled. While it is disabled, the section cannot be expanded. |
| Pre-Op Enabled / Pre-Op Disabled | Checks that the beam is clear before a tool change starts. Shown only while detection is enabled. A new profile starts with Pre-Op Enabled. |
| Signal Normal / Signal Inverted | Swaps how the input is read: a reading taken as beam blocked is taken as beam clear, and the other way round. If tool changes report the beam blocked when it is clear, or clear when it is blocked, switch it. A new profile starts with Signal Normal. |
Running the RapidChange ATC with tool detection disabled is not recommended in a regular workflow.
Fields
| Field | Description |
|---|---|
| Input | The controller input the IR sensor (yellow wire) is wired to. The list shows your controller's inputs, and the default is the first in the list. Where your controller addresses inputs by port and pin, the field is split into Input Port and Input Pin. |
| Z Zone 1 Offset | How far below Z Position the zone 1 check is made. Default 3 mm. |
| Z Zone 1 | Read-only: Z Position minus Z Zone 1 Offset. |
| Z Zone 2 Offset | How far above Z Position the zone 2 check is made. Default 3 mm. |
| Z Zone 2 | Read-only: Z Position plus Z Zone 2 Offset. |
Each offset must be between 0 and 4 mm. The zones are measured from the Z Position of the magazine's first pocket in Pocket Positions. When you find a new Z Position, the zones follow it and keep their offsets.
The Checks
| When | At | The beam must be | Meaning |
|---|---|---|---|
| After an unload | Z Zone 1 | clear | The nut has come off the spindle. |
| After a load | Z Zone 1 | blocked | A nut is on the spindle. |
| After a load | Z Zone 2 | clear | The nut is fully threaded, not caught on a thread. |
If an unload check fails, the unload is retried once before you are asked to finish it by hand. If a load check fails, the spindle moves to a safe height and the tool change stops with a message such as "Tool 3 failed zone 2. Manually load tool 3". Load the tool by hand, then continue: with Cycle Start, or with OK in the message box, depending on your controller.
With Pre-Op Enabled, a tool change that starts with the beam blocked stops and asks you to clear the obstruction. Depending on your controller, you then continue or the tool change is cancelled.
With tool detection Disabled, nothing is checked. Instead, the tool change stops after each unload and each load for you to confirm it worked.
Detection Zones
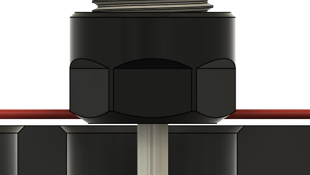
Zone 1 is the lower detection zone. A properly loaded tool breaks the beam at this height, while an empty spindle does not.
Z Zone 1 has more freedom of position than Z Zone 2.
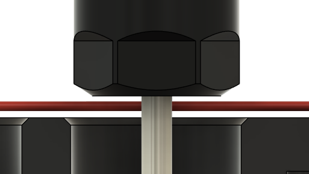
Zone 2 is the upper detection zone. A properly loaded tool clears the beam at this height, while a tool that failed to thread completely still breaks it.
Z Zone 2 has a small working range (2–3mm). If you see false failures when loading, the Z Zone 2 Offset may need adjustment.